A bearing bore may meet its size limit while remaining oval, tapered or barrel-shaped. In a robot joint, these form errors can change fit, preload and bearing life.
Roundness describes one cross-section; cylindricity evaluates the complete cylindrical surface. Both must be related to the specified datum and verified with a suitable method.
Bearing-seat risks
| Risk | Cause | Control |
|---|---|---|
| Bore becomes oval after release | Housing distortion from clamping | Limit force and compare clamped and free states |
| Diameter passes but bore is tapered | Tool deflection, uneven stock or thermal drift | Stabilize stock, tool overhang and temperature |
| Multiple bores are misaligned | Separate setups or changing references | Use a common setup or transferable datum system |
Separate size from form
Two-point diameter readings cannot prove full bore form. The drawing and inspection plan should state whether size, roundness, cylindricity, position or coaxiality controls the function.
Control the clamped and free states
Thin housings can be forced round by the fixture and spring back after release. Support stiff regions, limit force and include a free-state check before accepting the process.
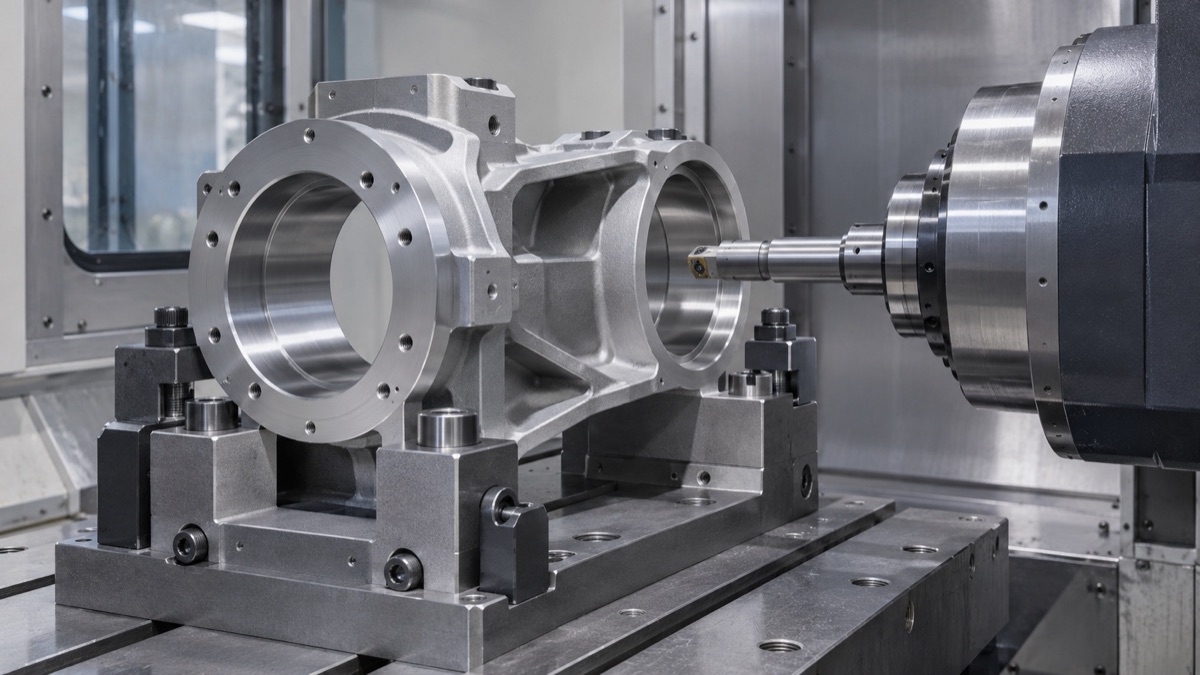
Rigid support, uniform stock and a common datum reduce bore-form and axis errors.
Use stable finishing conditions
Fine boring, reaming, grinding or honing should be selected by size, material and accuracy. Uniform finish stock, short overhang, controlled wear and stable thermal conditions reduce taper and lobing.
Keep related bores on one datum chain
When several bearings define a joint axis, machine or transfer them from a verified common reference. Independent local datums can produce individually good bores that do not assemble on one axis.
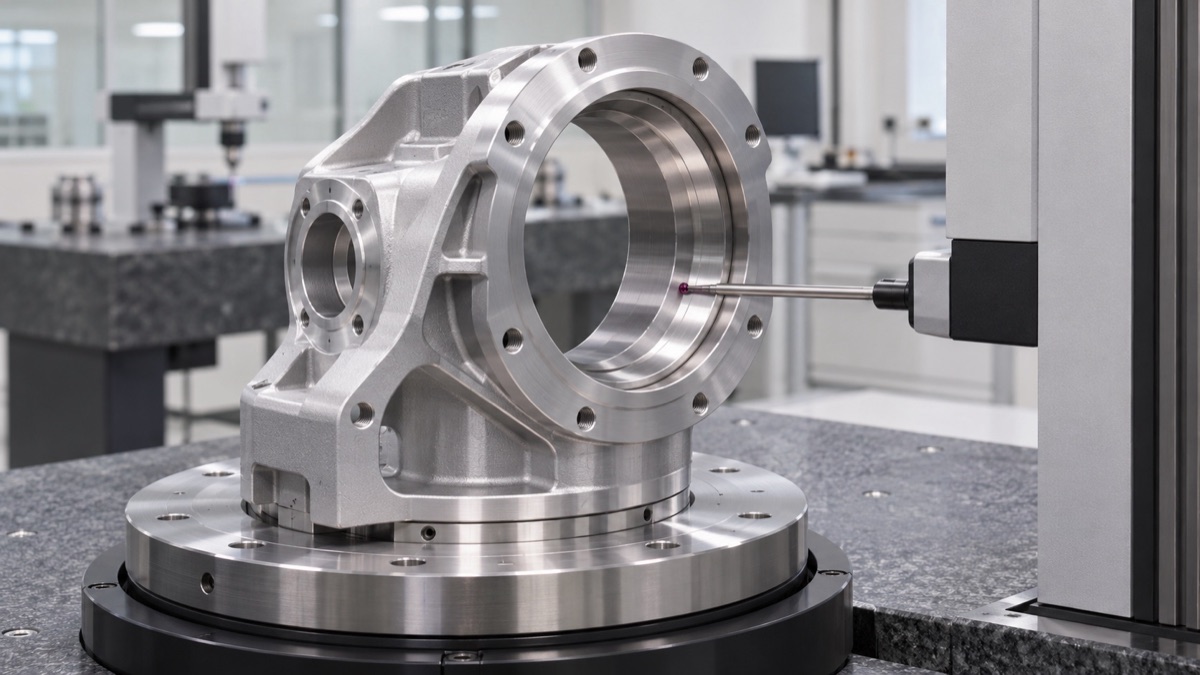
Multiple sections or scanning are needed to distinguish roundness, taper and full cylindricity.
Measure enough of the surface
Use multiple cross-sections or a suitable scan, with documented filtering, probe and alignment settings. Functional assembly checks complement measurement but do not replace geometric evidence.
Summary
Bearing-seat quality requires control of size, form and axis relationships. A stable fixture, consistent finishing stock and a measurement plan that covers the full bore are essential.
FAQ
Are roundness and coaxiality the same?
No. Roundness is the form of one circular section; coaxiality concerns the relationship between axes.
Can a bore gauge measure cylindricity?
It can show diameter variation at selected points but normally cannot establish the complete cylindricity surface.
Does an easy bearing press prove the bore is correct?
No. Assembly feel cannot isolate size, form, surface, bearing variation and pressing alignment.
Ready to get a quote for your CNC machined parts?
Submit your engineering drawings to qiancj@oemach.com. We support prototype sampling and small-batch production with strict tolerance control.