An RV reducer's low-speed stage is a system of cycloidal discs, eccentric motion, pins, bearings and clearance. A highly accurate profile can still produce torque variation if its relationship to the eccentric and pin system is wrong.
The approved digital geometry, machining program and inspection program must share one revision, followed by paired assembly evidence across a full rotation.
Combined errors and controls
| Problem | Cause | Evidence |
|---|---|---|
| High transmission error | Profile, modification and eccentric errors combine | Profile deviation, eccentricity and error curve |
| Uneven pin contact | Pin position, diameter or housing form varies | Pattern position, pin size and contact pattern |
| Good parts bind when paired | Clearance not validated in combination | Pair ID, starting torque and full-cycle variation |
Treat the reducer as one functional chain
Profile deviation, pin diameter and position, eccentricity and bearing clearance jointly affect contact and transmission. Datum relationships matter as much as each feature's individual accuracy.
Keep digital profile versions synchronized
Cycloidal modification means the nominal contour is project-specific. Design model, compensation, machining and metrology software must use the same approved data and change record.
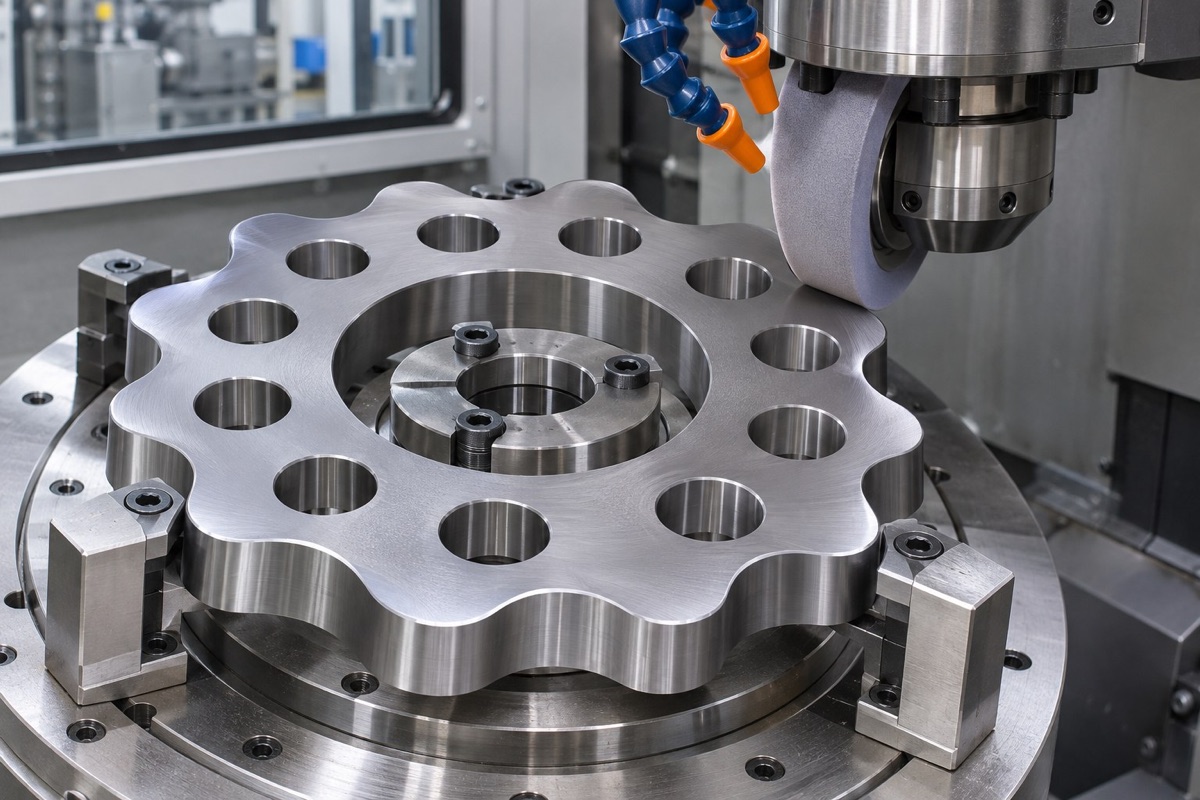
The approved digital profile must remain aligned with eccentric bores and output-hole features.
Organize machining around eccentric datums
After heat treatment, verify distortion and restore references before profile finishing. Complete related bores in high-repeatability setups so individually good features remain correctly located.
Control the complete pin-wheel assembly
Pin diameter alone is insufficient. Evaluate pin-hole distribution around a common center, housing form, face condition and the assembled radial pattern.
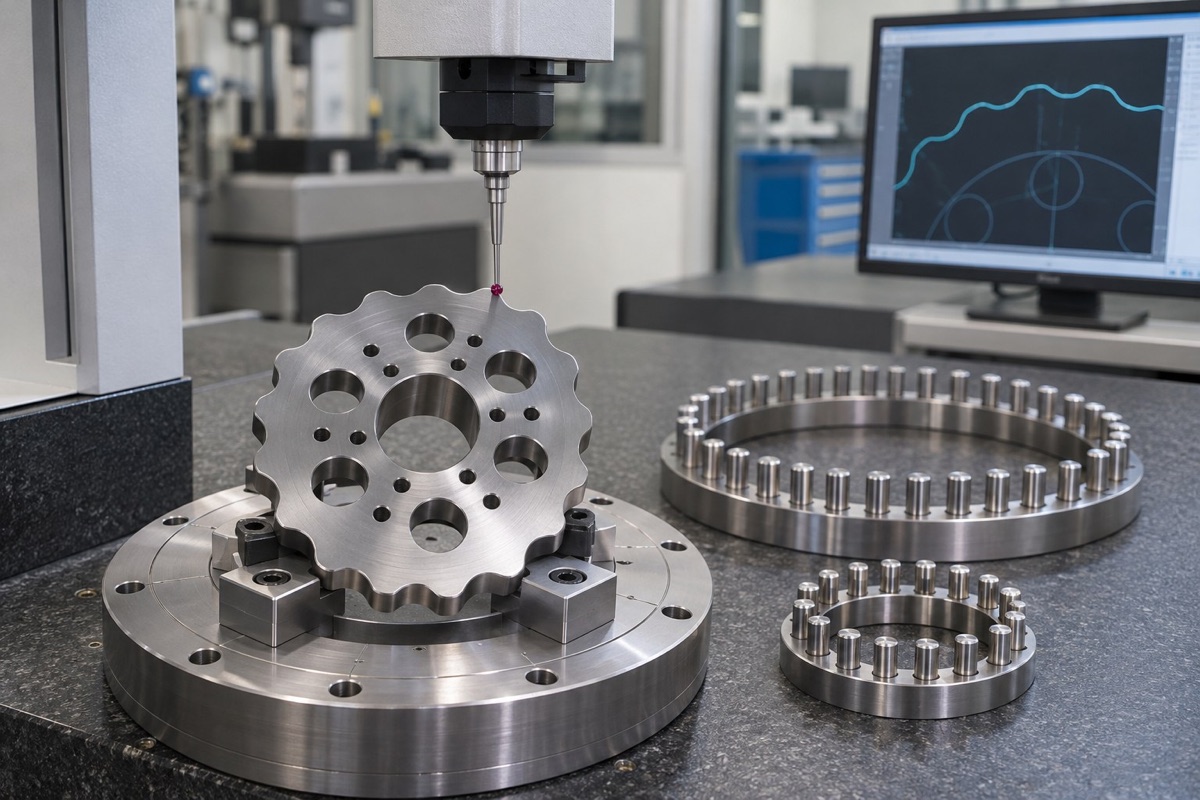
Single-part inspection should be supplemented by contact, starting-torque and full-rotation checks.
Combine metrology with paired testing
Fix point density, fitting datum and filtering for profile measurement. Number paired components and record contact, starting torque and full-rotation variation to locate functional errors.
Summary
RV reducer accuracy is a system result. Synchronized digital data, common eccentric datums, complete pin-wheel control and traceable paired testing are all required.
FAQ
Can a cycloidal outline be accepted with ordinary profile tolerance?
A profile method can be used only with the approved theoretical contour, datum scheme and evaluation algorithm.
Why is contact uneven when every pin diameter passes?
Pin-hole position, housing roundness, eccentricity and assembly clearance also affect contact.
Can part inspection replace transmission testing?
No. Part data locates manufacturing error; combined testing validates actual meshing performance.
Ready to get a quote for your CNC machined parts?
Submit your engineering drawings to qiancj@oemach.com. We support prototype sampling and small-batch production with strict tolerance control.